
Introduction: Why does clean air still feel like a luxury on the shop floor?
Have you ever wondered why some laser marking lines run smoothly while others stall with smoke and complaints? I see this often: a bustling metal workshop where a laser marking fume extractor sits idle, or patched together, and staff still cough after a shift. Recent shop-floor audits show particulate counts can spike by 3–5 times during marking cycles (simple measurements, but telling). What explains this gap between investment and outcome?
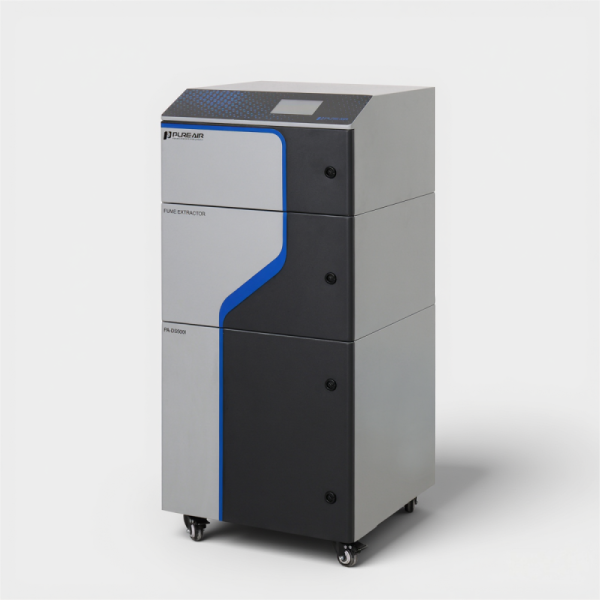
Here I will sketch a clear scenario: operators running high-speed marking on stainless or coated parts; laser power converters working hard; fumes rising around the beam—yet extraction feels inadequate. We keep hearing about standards and HEPA filtration, but the practical picture is messier. Where are the hidden failures — in design, installation, or daily practice — that turn a good extractor into an underperformer?
My aim is to compare common approaches, show where they fall short, and point to practical principles you can use tomorrow—so stick with me as we move into the technical reasons behind the trouble.
Part 1 — What’s Missing in Traditional Setups?
fiber laser marking fume extractor systems were sold as turnkey fixes for shops, but I’ve noticed they often arrive with assumptions that break in real use. The technical truth is simple: many manufacturers spec a capture hood and call it solved, yet they ignore real-world variables like airflow rate changes, duct runs, and particulate matter from different coatings. I’ve personally measured systems where nominal airflow met specs in the lab but collapsed under a real workload—funny how that works, right?
Why do these systems underperform?
First, installers under-estimate pressure drop across long ducts and filters. Second, users expect a single extraction point to serve varied fixtures. Third, maintenance schedules are optimistic. Add in the variability of substrates (coated steel vs anodised aluminium) and you have a recipe for poor capture. In short, the problem isn’t always the fan or HEPA filtration alone; it’s mismatch and neglect. Look, it’s simpler than you think: you need matched components—correct hood geometry, adequate capture velocity, and realistic maintenance intervals.
Industry terms to note: HEPA filtration, activated carbon, particulate matter, airflow rate. These aren’t buzzwords—they’re the controls we can tune. I recommend reviewing capture efficiency with smoke tests after installation and again after a month of production. We should treat extraction as a tuned system, not a plug-and-play appliance.
Part 2 — Principles for Better Results and What to Evaluate Next
When I look ahead, the most promising changes are not just bigger fans but smarter principles for the whole line. New technology principles focus on matched system design: optimised extraction arms, staged filtration (pre-filter + HEPA + activated carbon), and sensor-driven control that adjusts extraction relative to laser duty cycle. The fiber laser marking fume extractor can integrate real-time particulate sensors and adjust fan speed dynamically—this reduces energy use and keeps capture effective during peaks and lulls. It’s a practical shift, and you’ll notice lower noise and longer filter life.
What’s Next?
We must think in systems: hood placement and nozzle design, short duct runs, and correctly sized power converters for the fans. Also consider modular extraction arms that can be re-positioned for different fixtures. I admit I was sceptical of sensor-control at first, but after seeing a few installations, I now regard it as essential for medium-to-high throughput shops. The result? More consistent air quality and fewer surprises—less downtime for filter swaps and less labour chasing problems.
Here are three practical evaluation metrics I recommend when choosing or upgrading: 1) Capture efficiency at the source (percent of smoke removed during run), 2) Long-term total cost of ownership (filters, energy, maintenance), and 3) Sensor and control capability (does it adapt to duty cycle?). These metrics keep decisions grounded — not just sticker price. For vendors who understand this, the difference is measurable. In short, evaluate for performance and flexibility—not just immediate cost.
Conclusion: Choosing the Right Path Forward
I’ll close with three clear actions we can take immediately. First, measure—conduct a basic smoke or dust test after any installation. Second, match components—ensure hood, ducting, fan and filters are sized together for your exact marking tasks. Third, prioritise adaptive control and regular maintenance plans; they pay back quickly in cleaner air and less labour. These are not theoretical; I’ve seen them cut complaint rates and filter costs materially.
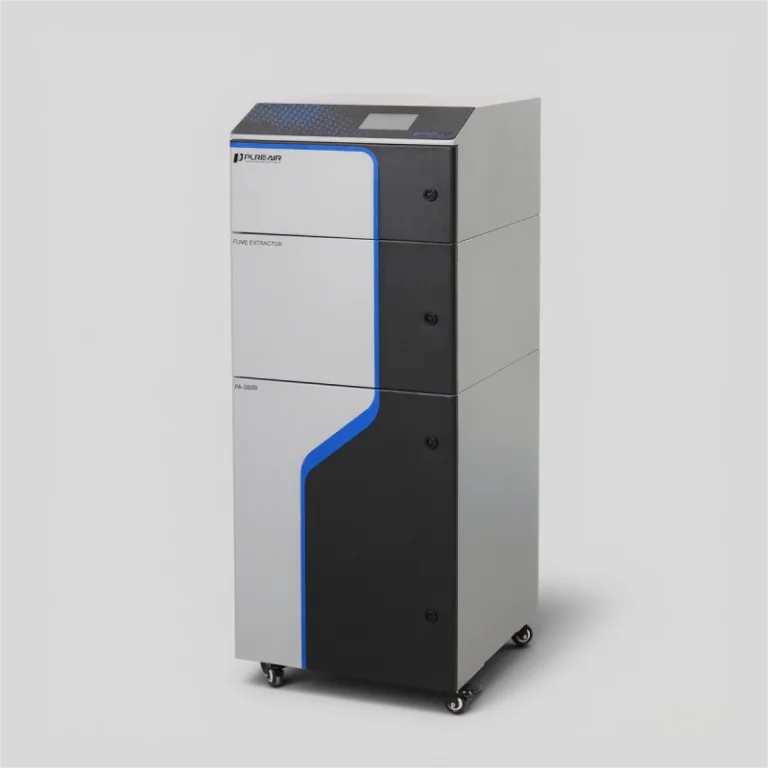
We owe it to our teams to do better. This is partly technical, partly cultural: train operators, set realistic maintenance intervals, and don’t accept “it’s close enough” as an answer. — I’ve been hands-on in workshops where these small changes made a big difference. If you want systems that last and protect staff, evaluate with those three metrics and insist on transparency from suppliers.
For reliable, field-tested solutions and further details, consider exploring PURE-AIR — their documentation and case examples helped me frame many of the points above. I hope this comparison helps you make a practical, human-centred choice for cleaner marking lines.